Oem Egg Farm Packer Machine
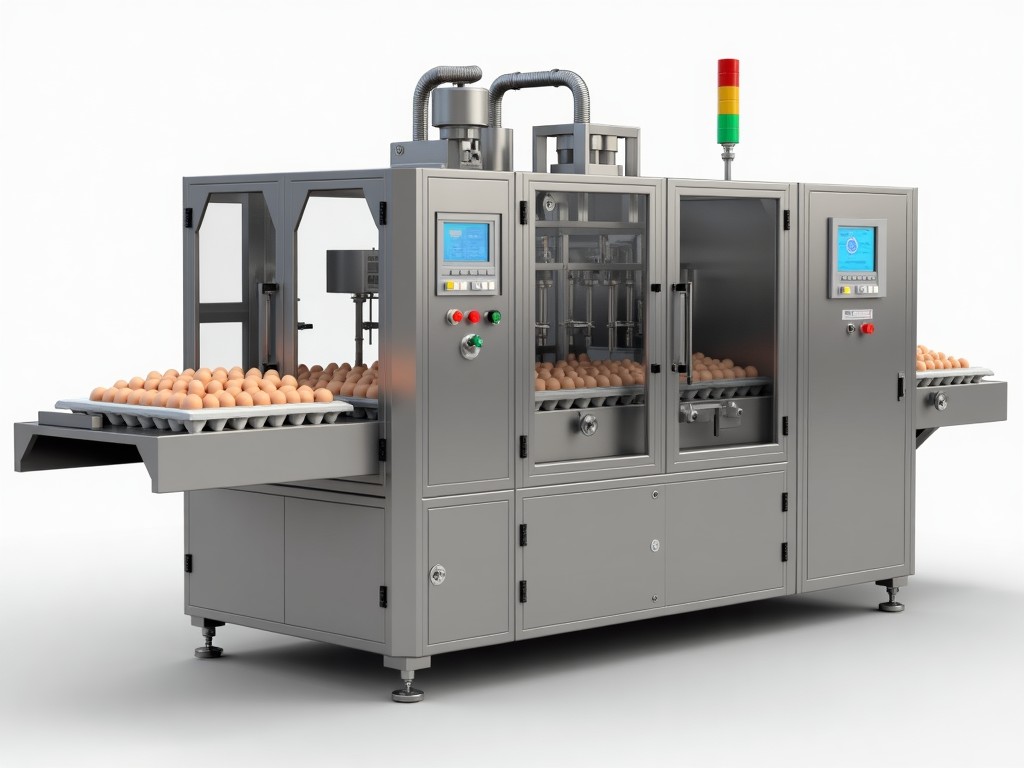
OEM Egg Farm Packer Machine: Integrated Automated Packing Solutions
Scaling egg production requires a delicate balance between high-throughput processing and product integrity. OEM egg farm packer machines are designed to integrate directly into existing agricultural workflows, providing a transition from manual-intensive sorting to fully automated lines. By focusing on modular architecture, these systems allow manufacturers to offer customized hardware configurations that meet varying regional grading standards and farm-specific packaging requirements.
The engineering philosophy behind these packers centers on the reduction of mechanical stress during the transport phase. Unlike generic conveyor systems, modern OEM solutions utilize servo-driven synchronization and soft-touch contact surfaces to ensure that eggshells remain intact, even at peak operational speeds.
Technical Specifications and Parameters
| Parameter | Typical Values | Customizable Options |
|---|---|---|
| Production Capacity | 2,000 - 8,000 eggs/hour | Adjustable via multi-line configuration |
| Egg Weight Range | 35g - 75g | High-precision sensors for specialty eggs |
| Construction Material | SUS304 Stainless Steel | SUS316 for high-wash environments |
| Control System | PLC / Schneider | Custom HMI interface and software |
| Power Requirement | 380V / 3-Phase | Voltage-specific transformers available |
Engineering Logic and Core Features
The core functionality of an OEM egg packer lies in its precision grading mechanism. By utilizing high-speed load cells integrated with vibrating feeders, the system evaluates individual egg weights with sub-gram accuracy. This precision prevents the "clumping" effect that often leads to mechanical breakage in lower-speed mechanical systems.
- Servo-Driven Transport: Eliminates jerky movements associated with traditional belt drives, ensuring a smooth flow into the packing trays.
- Modular Line Design: Allows for the seamless addition of cleaning, disinfecting, or labeling modules without redesigning the entire chassis.
- Food-Grade Compliance: All contact surfaces are constructed from non-porous materials that meet or exceed stringent international food safety standards.
- Smart HMI Interface: Provides real-time data on production rates, breakage percentages, and diagnostic alerts for preventative maintenance.
Operational efficiency is another priority for OEM partners. The internal machinery is designed with easy-access panels and quick-release components, which significantly reduces the time required for daily sanitation cycles. This focus on downtime-minimization engineering ensures that the packing line remains operational during peak harvest seasons.
Customization Options for OEM Partners
True OEM partnerships require the ability to adapt hardware to specific market demands. We provide a variety of customization paths that allow distributors to differentiate their offering to the end-user.
Tray Configuration Flexibility
The packing head can be configured to handle various tray types, including:
- Standard pulp trays (30-count)
- Molded plastic PET trays
- Eco-friendly cardboard trays for retail export
- Custom-sized configurations (e.g., 6-count, 12-count, or 18-count)
Beyond physical hardware, the software layer can be white-labeled. This includes custom branding on the HMI screens, localized language support, and API integration for the farm's existing enterprise resource planning (ERP) software.
Industrial Applications
Automated egg packers are deployed across diverse environments where labor costs and consistency are critical. These machines are not merely tools but are central components of a modern agricultural supply chain.
In large-scale commercial farm operations, these machines handle the volume of thousands of eggs daily while maintaining strict uniform grading for retail contracts. Conversely, for **specialized organic producers**, the precision of the sensors ensures that smaller, high-value eggs are handled without the damage often seen in older mechanical systems. Furthermore, **export facilities** utilize the modular nature of these packers to integrate automated weighing, labeling, and coding stations required for international shipping compliance.
Quality Control and Inspection
To ensure long-term reliability, every OEM egg packer undergoes a rigorous testing protocol before shipment. This includes stress-testing the transport mechanisms at 110% of rated capacity for 48 hours to identify potential mechanical fatigue points.
We also calibrate the load cells using certified weights to ensure the grading accuracy remains consistent over thousands of cycles. Material verification is performed for all stainless steel components, confirming that the machine will withstand the corrosive nature of industrial egg cleaning agents.
Are you looking to develop a custom packing solution for your farm or distribution product line?
Request Technical Data and Quotation


