B2B High Capacity Egg Farm Packing Machine
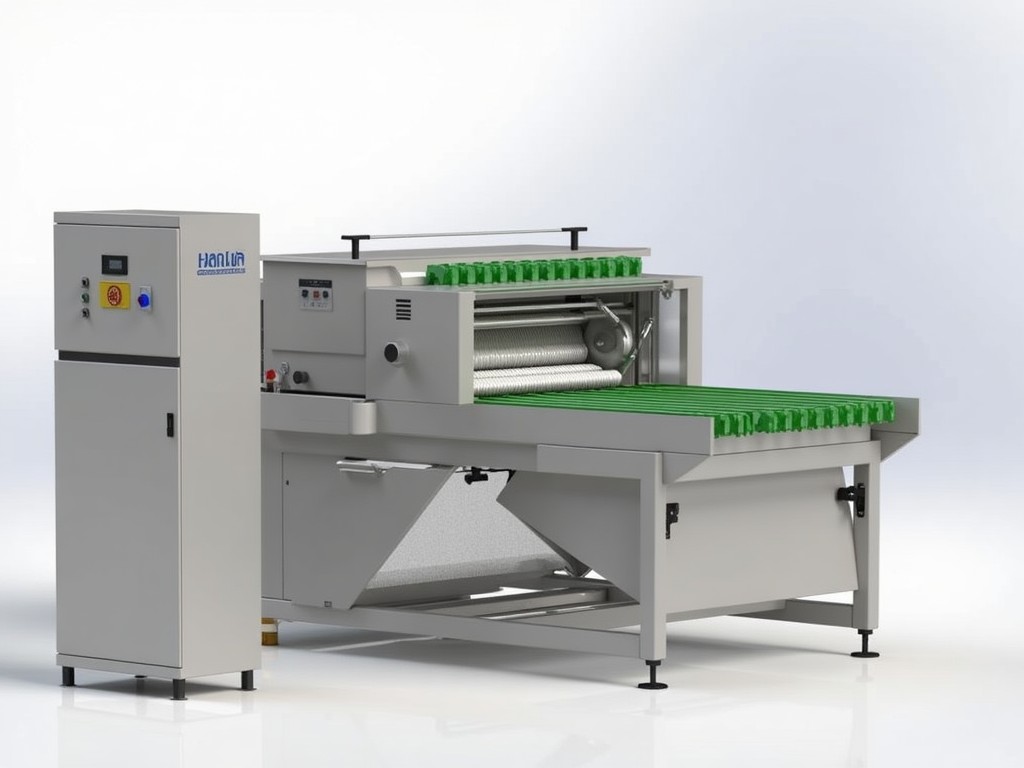
B2B High Capacity Egg Farm Packing Machine
This equipment is designed for continuous grading, counting, and packaging of table eggs in large‑scale production facilities. It integrates a vibratory feeder, vision‑based sorting system, and a servo‑driven carton loader to achieve throughput rates suitable for farms processing tens of thousands of eggs per hour.
Technical Specifications
| Parameter | Typical Value | Notes |
|---|---|---|
| Maximum Throughput | 30,000 eggs/hour | Adjustable via lane speed and feeder rate |
| Egg Size Range | 40 mm – 65 mm diameter | Customizable guides available |
| Frame Material | Stainless steel 304, 2 mm thickness | Corrosion resistant for wash‑down environments |
| Drive System | Servo motors, total 1.5 kW | Precise positioning, low maintenance |
| Control | PLC with HMI touchscreen (7‑inch) | Recipe storage for multiple carton types |
| Power Supply | 380 V ± 10 %, 3‑phase, 50/60 Hz | Optional 460 V version |
| Footprint (L × W × H) | 2,200 mm × 1,200 mm × 1,800 mm | Includes infeed and outfeed conveyors |
Key Functional Features
- Vibratory feeder with adjustable amplitude ensures consistent singulation without shell damage.
- High‑speed vision system (2 MP camera, 500 fps) detects cracks, stains, and size variations; reject rate <0.2 %.
- Servo‑driven carton loader places eggs into trays with positional accuracy ±0.5 mm, reducing breakage.
- Modular lane configuration (2‑4 lanes) allows line re‑balancing for different pack sizes (6, 12, 18, 30 eggs per carton).
- Sanitary design includes CIP‑spray nozzles and smooth surfaces with ≤0.8 µm Ra finish to meet food‑grade standards.
- Energy recovery brake on outfeed conveyor reduces peak power draw by ~15 % during cyclic operation.
Applications in Egg Production
Facilities that produce >250,000 eggs per day benefit from continuous packing because manual handling creates bottlenecks and increases labor‑related variability. The machine’s vision‑based grading removes defective eggs upstream, which improves downstream carton seal integrity and reduces waste in retail channels.
Integrated with upstream washing and drying units, the packing line can operate as a closed loop, maintaining a constant temperature profile that prevents condensation on shells—a critical factor for preserving microbial safety during storage.
For farms that supply multiple carton formats (e.g., retail trays, bulk flats, and export crates), the quick‑change lane system allows a format switch in under eight minutes, minimizing downtime between product runs.
Frequently Asked Questions
- Can the lane width be adjusted for different egg sizes? Yes, the guide rails are motorized and adjustable from 38 mm to 70 mm via the HMI.
- What information is required for a quotation? Required data include target eggs per hour, preferred carton dimensions, facility power specifications, and any required integration with existing conveyors.
- Which materials are available for contact surfaces? All egg‑contact parts are supplied in 304 stainless steel; optional 316L for high‑chloride environments.
- How is quality inspected during operation? The system logs reject counts, size distribution, and average placement error; data can be exported via Ethernet for SPC analysis.
- What packaging options are supported? The loader accommodates cardboard trays, PET clamshells, and reusable plastic crates with adjustable nest depth.
- How are export shipments protected? The machine includes a vibration‑isolating frame and optional desiccant‑sealed housing for transit to humid climates.
- What is the typical lead time? Standard configuration ships within 10‑12 weeks after receipt of purchase order; custom lane counts may extend to 16 weeks.
Next Steps
To discuss how this packing system can be matched to your farm’s output profile, please provide your hourly egg volume, preferred carton size, and facility layout constraints. Our engineering team will return a preliminary layout drawing and power budget within two business days.



