Factory Direct Egg Vacuum Handling Machine
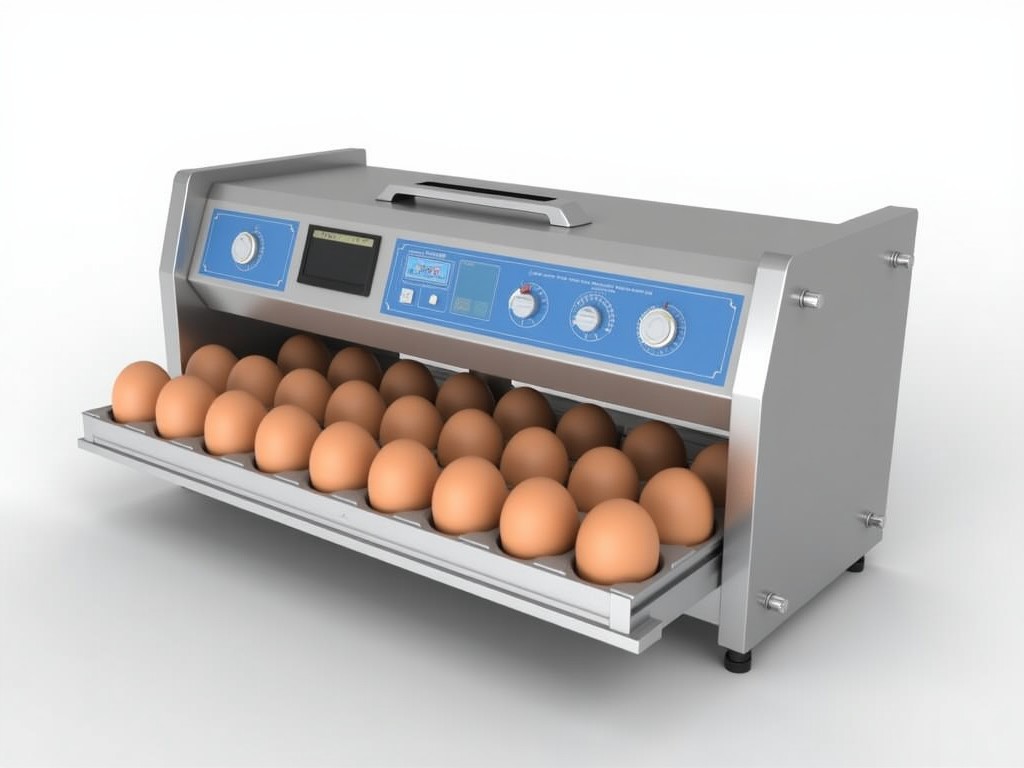
Factory Direct Egg Vacuum Handling Machine
This equipment moves individual eggs from trays to processing stations using a regulated vacuum suction system. By avoiding mechanical grippers, it reduces shell breakage and maintains product hygiene throughout the line.
The suction head incorporates an array of food‑grade silicone cups arranged to match standard egg tray pitch. A programmable vacuum pump generates a pressure differential of approximately −0.8 bar, sufficient to lift a 60 g egg without deformation. Cycle time is controlled by a PLC with adjustable dwell settings ranging from 0.3 s to 1.2 s per transfer, allowing synchronization with varying line speeds. Sensors detect cup‑egg contact and vacuum level, triggering a release signal only when both parameters are within preset thresholds. All moving components are mounted on a stainless‑steel frame rated for wash‑down environments (IP66).
Key Specifications
| Parameter | Typical Value | Notes / Options |
|---|---|---|
| Maximum payload per cup | 60 g (standard egg) | Up to 80 g with reinforced cup material |
| Vacuum range | −0.4 bar to −1.0 bar | Adjustable via regulator |
| Cycle rate | Up to 80 cycles/min | Dependent on dwell time setting |
| Power supply | 380 V ± 10 % 3‑phase, 50/60 Hz | Optional 220 V configuration |
| Frame material | AISI 304 stainless steel | AISI 316 available for corrosive media |
| Control interface | PLC with touch‑screen HMI | Profibus, EtherNet/IP, Modbus TCP options |
Typical Applications
In egg breaking lines, the machine transfers eggs from loading trays to the cracker station with minimal contact, which reduces the incidence of hairline fractures that can lead to microbial contamination. The non‑mechanical handling also eliminates the need for lubricants, simplifying cleaning validation for food‑grade facilities. Beyond primary breaking, the same principle applies to conveying eggs to inspection stations, where orientation consistency is critical for automated vision systems. Because suction force scales with egg weight, the equipment accommodates both table‑egg and specialty‑egg sizes without mechanical re‑tooling. Installations in poultry processing plants have reported a 15 % increase in usable yield after switching from mechanical pick‑and‑place to vacuum handling.
Customization Options
- Number of suction heads (single‑lane to multi‑lane configurations)
- Cup material: food‑grade silicone, FDA‑approved polyurethane, or antimicrobial‑treated elastomer
- Mounting height and reach adjustments to match varying conveyor elevations
- Integration kits for existing PLC architectures (I/O mapping, safety relay interfaces)
- Surface finishes: polished Ra 0.4 µm for hygienic zones or brushed for structural areas
Each option is evaluated against the customer’s line layout, sanitation protocol, and expected throughput to ensure that the final solution meets both functional and regulatory requirements. Design changes are documented in a configuration sheet that includes revised vacuum settings, cup spacing, and load calculations. Prototypes can be run on‑site for validation before final fabrication.
Quality Assurance
Manufacturing follows ISO 9001 procedures with in‑process inspections of weld integrity, surface roughness, and cup elasticity. Final testing includes a 100 % vacuum leak check using a mass‑flow sensor, a functional run‑test at maximum rated speed, and a sanitation‑compatibility rinse cycle. Test records are retained for traceability and are available to the buyer upon request. All components that contact eggs are certified to meet EC 1935/2004 and FDA 21 CFR 177.2600 standards.



