Factory Supply Egg Grading Station For Sale
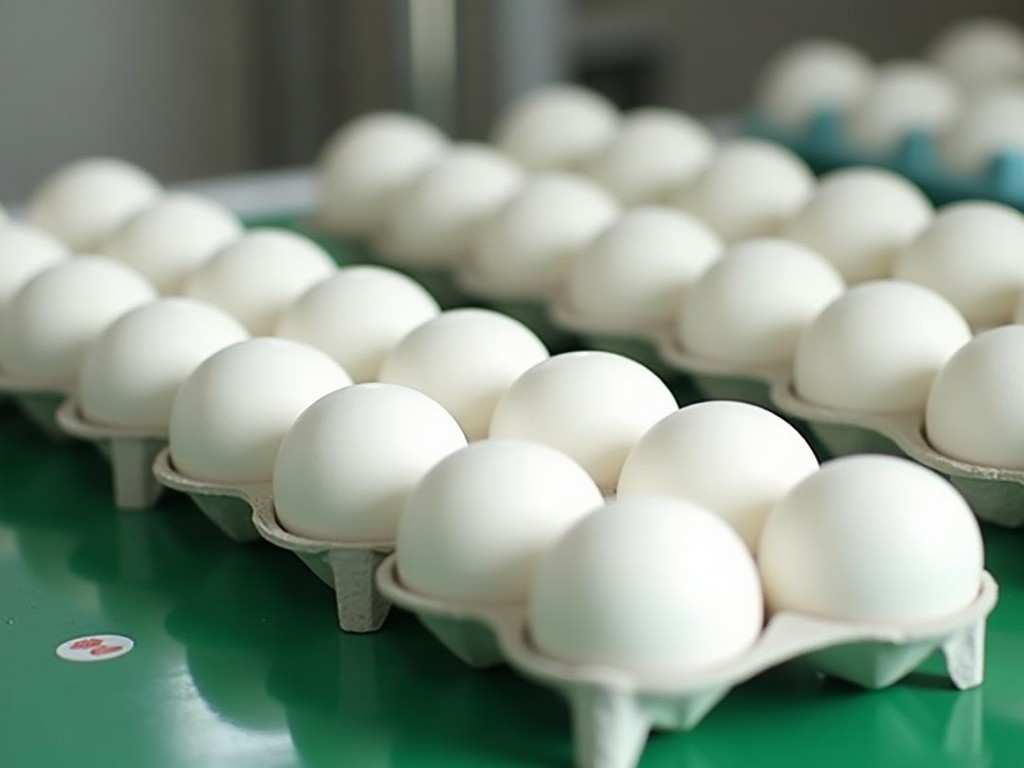
Factory Supply egg grading station for sale
Automated egg grading stations transition facilities from manual inspection to high-throughput industrial processing. These systems integrate weight-based sensors and optical inspection to ensure every unit meets specific weight-classing requirements before distribution. By replacing manual sorting, facilities can significantly reduce human error and maintain consistent quality standards across the supply chain.
Technical Specifications
| Parameter | Typical Values / Customizable Options |
|---|---|
| Processing Capacity | 2,000 - 20,000 eggs per hour (depending on configuration) |
| Weight Accuracy | ±0.5g precision |
| Material Options | SUS 304 Stainless Steel, Galvanized Steel, or Food-grade Aluminum |
| Control System | PLC-based logic with HMI Touch Interface |
| Power Requirement | 220V/380V, 50/60Hz |
| Grading Method | Weight-based, Optical-based, or Combination |
Key Components and Engineering
The mechanical integrity of a grading station relies on the synchronization of physical transport and electronic sensing. Each component is selected to minimize mechanical stress on the product while maximizing data acquisition speed.
High-Precision Load Cells
Weight measurement utilizes strain-gauge load cells integrated into the roller conveyor sections. These sensors calculate weight in milliseconds, allowing the PLC to divert eggs into the correct channels without slowing the line speed. High-frequency data sampling ensures accuracy is maintained even in high-volume environments.
Optical Inspection Modules
Infrared and high-resolution optical sensors detect surface defects such as cracks, blood spots, or discoloration. By processing visual data in real-time, the system flags rejects that do not meet aesthetic or safety standards before reaching the packaging stage.
Roller Belt Transport
The transport path utilizes polyurethane-coated rollers designed to provide gentle lateral movement. This design prevents shell fractures often associated with traditional friction belts, maintaining the structural integrity of the eggs during the vibration-heavy sorting process.
Industrial Applications
Egg grading stations are deployed across various sectors of the poultry industry where consistency and hygiene are primary operational drivers.
- Large-Scale Poultry Operations: Handling massive daily volumes from farm-gate to streamline sorting for distribution hubs.
- Export Grading Centers: Ensuring precise weight-classing to meet international trade regulations and consumer specifications.
- Processed Food Plants: Pre-sorting eggs for liquid egg production where shell integrity and contaminant control are critical.
Customization and Scalability
Engineering flexibility allows for modular configurations that fit specific facility layouts and production targets. Systems can be scaled from single-line units to multi-line integrated processing plants.
Material selection is based on the operational environment; for wash-down facilities, SUS 304 stainless steel is standard to resist corrosion from frequent cleaning agents. Conveyor widths and the number of output channels are adjusted to accommodate different egg sizes and final packaging requirements.
Frequently Asked Questions
Can the dimensions be customized to fit existing floor plans?
Yes, the modular design allows for varying conveyor lengths and height configurations to be adjusted based on specific spatial constraints.
What is the typical production lead time for a custom order?
Production typically ranges from 4 to 8 weeks depending on the complexity of the optical sensors and material specifications.
What materials are available for high-humidity environments?
Full SUS 304 stainless steel construction is recommended for environments with high humidity or high-pressure wash-downs.
Require a technical data sheet or a custom quotation for your facility?
Request Technical Consultation


