Oem Egg Robotic End Of Line Packaging Machine
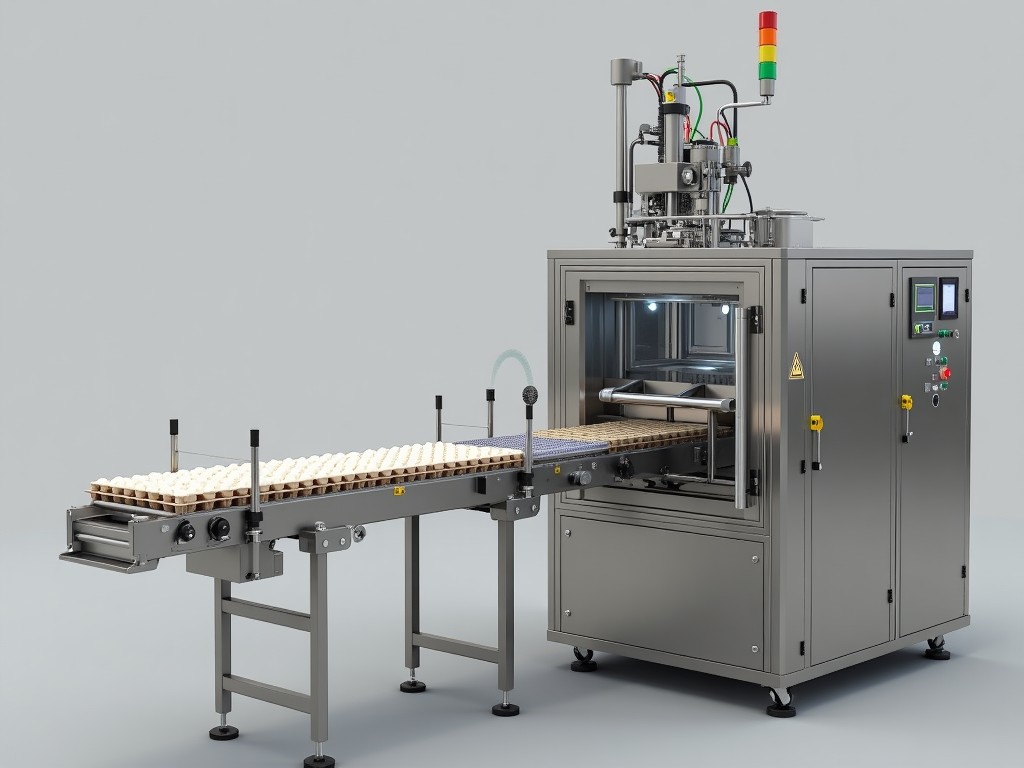
OEM Egg Robotic End-of-Line Packaging Machine
This solution integrates a six‑axis articulated robot with a high‑speed vision system and a compliant soft‑gripper end effector to transfer eggs from the upstream conveyor into cartons, trays, or flow‑wrap packages at line speeds typical of medium‑ to high‑volume poultry processing.
Core Technology
The robot provides a repeatability of ±0.02 mm and a maximum reach of 1.3 m, enabling precise placement across multiple carton formats without re‑tooling. A 2‑MPixel camera with LED illumination operates at 500 fps, feeding position data to the controller at 1 kHz for real‑time trajectory correction.
The end effector uses silicone‑based fingers with adjustable grip force (0.5 N‑2.0 N) to handle eggs of varying shell strength while maintaining a cycle time under 0.8 s per pick‑place operation.
Key Performance Parameters
| Parameter | Typical Value | Notes |
|---|---|---|
| Maximum Payload | 1.5 kg | Includes egg weight plus gripper mass |
| Reach (Horizontal) | 1.3 m | Covers multiple carton lanes |
| Repeatability | ±0.02 mm | ISO 9283 compliant |
| Cycle Time (Pick‑Place) | 0.8 s | Includes vision processing |
| Power Consumption | 1.2 kW (peak) | 380 V / 3 phase |
| Footprint (L × W × H) | 1.6 m × 0.9 m × 2.1 m | Includes safety guarding |
Typical Applications
In line‑loading operations, the machine receives eggs from a grading conveyor, orients them according to customer‑specified position (point‑up or point‑down), and places them into pre‑formed cartons at rates up to 450 eggs per minute. The vision system detects misshapen or cracked shells and diverts those units to a reject stream, reducing downstream waste.
For tray‑based packaging, the robot stacks eggs in a 2 × 5 or 3 × 6 matrix with a placement tolerance of ±0.5 mm, ensuring consistent layer alignment for automated sealing. The soft‑gripper design prevents shell fracture even when handling eggs stored at 4 °C.
The system can be adapted to flow‑wrap lines by attaching a custom suction‑cup module that seals individual eggs in film pouches, maintaining a seal integrity of >95 % at 200 ppm oxygen.
Customization Options
Reach and payload can be scaled by selecting alternative robot models (e.g., 700 mm reach, 0.8 kg payload) without changing the core control architecture. End effector geometries are interchangeable to accommodate different egg sizes (from 45 g to 70 g) or specialty products such as duck or quail eggs.
Vision lighting can be switched between broadband LED and narrow‑band infrared to improve contrast on colored or speckled shells. Software licenses include optional modules for barcode verification, weight checking, and data logging to MES systems via OPC‑UA.
Mechanical interfaces support multiple mounting standards (ISO 9409‑1‑50‑4‑M6, ISO 9409‑1‑80‑6‑M8) and can be configured for floor‑mount, ceiling‑suspended, or side‑mounted installations depending on plant layout.
Integration & Installation
The controller communicates over EtherCAT with cycle times of 250 µs, allowing synchronization with existing conveyor encoders and pneumatic actuators. A standard safety scanner (PLd, Category 3) provides collaborative operation when risk assessment permits, otherwise a safety fence with interlock switches is supplied.
Installation typically requires two days for mechanical anchoring, electrical termination, and initial calibration. Factory acceptance testing includes a 30‑minute run at 100 % line speed with statistical process control charts for placement error and reject rate.
Spare parts kits (gripper set, camera lens, cable harnesses) are available for quick‑change maintenance, reducing mean time to repair to under 30 minutes.
Quality Assurance & Testing
Each unit undergoes a 72‑hour soak test at rated load to verify thermal stability of servo drives and controller boards. Vision system accuracy is validated using a calibrated grid target with measurement uncertainty <0.01 mm.
Functional testing includes 10 000 consecutive pick‑place cycles with force feedback monitoring to ensure grip force remains within the specified 0.5 N‑2.0 N band. Documentation provides traceability of critical components (serial numbers, material certifications) per ISO 9001:2015.
Optional third‑party verification (e.g., CE, UL) can be arranged upon request, with test reports delivered alongside the equipment.
FAQ
Can the robot be reprogrammed for different package formats?
Yes. The motion program is stored in the controller and can be edited via the teach pendant or offline software. Changing carton dimensions typically requires updating a few position points and adjusting the gripper open/close timing, which can be completed in under two hours.
What information is needed for a quotation?
We require line speed (eggs per minute), carton or tray dimensions, egg weight range, available electrical supply (voltage, phase), and any environmental constraints (temperature, washdown rating). Providing a layout sketch helps optimize mounting and safety guarding.
Are there options for wash‑down or hygienic designs?
Stainless‑steel (AISI 304) covers and IP65‑rated motor enclosures are available for zones requiring regular cleaning. All cables can be supplied with halogen‑free, PUR jackets resistant to cleaning agents.
Next Steps
To discuss how this machine can be tailored to your specific production line, please reach out for a technical consultation.
Contact Our Engineering Team


